Categories
Extrusion Welders and Hot Air Blowers
Extrusion welding melts and extrudes the welding rod inside the gun and lays it onto a surface preheated with hot air; it is the method used on thick-walled sheet, tanks, pools and fabricated parts. The catalogue holds the Stargun UNO, LINK, K-SB and SOLO guns (1-6.2 kg/h), hot air blowers, and shoe and carrying accessories.
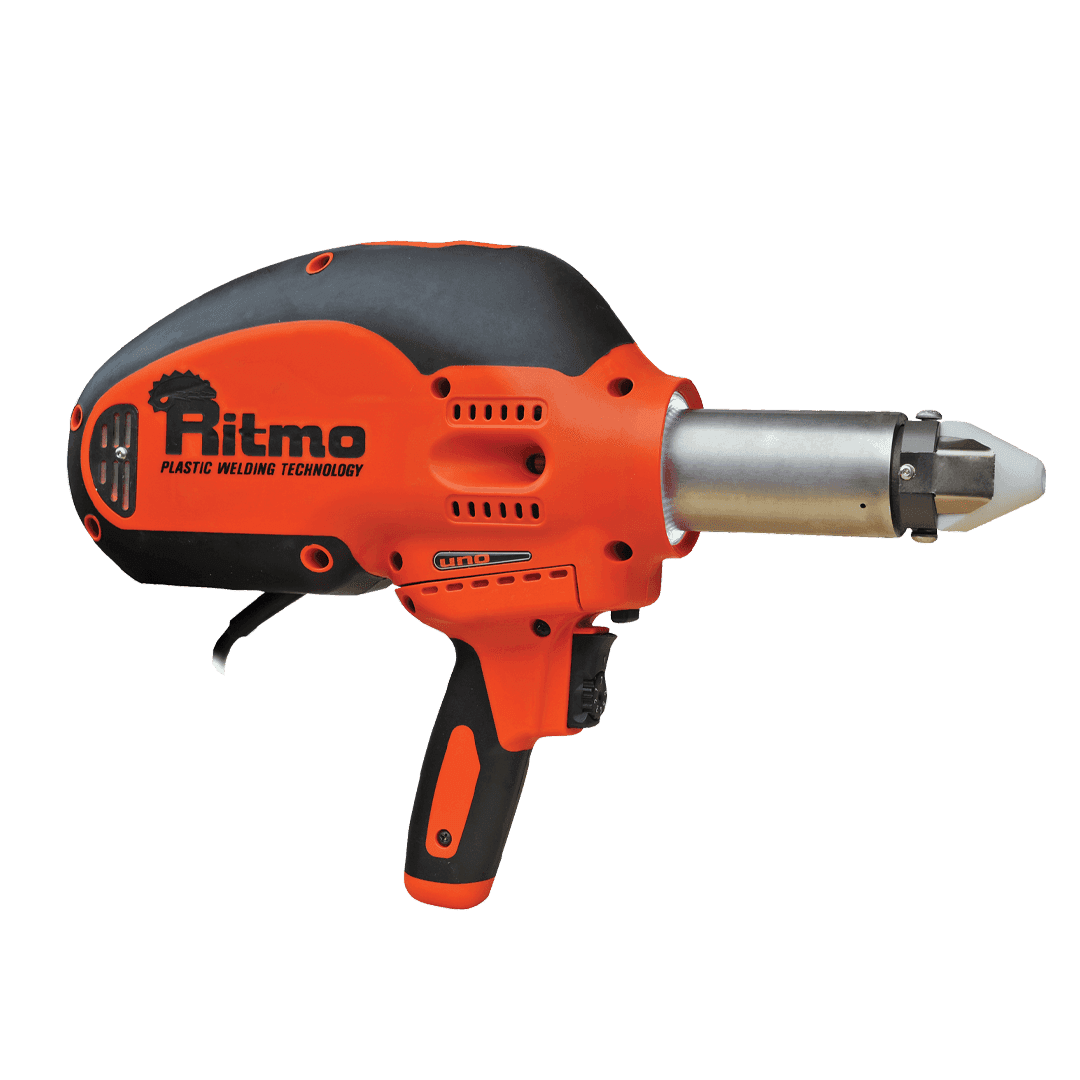
Ritmo Stargun UNO Extrusion Welder 1 kg/h
Ritmo · Extrusion Welders and Hot Air Blowers
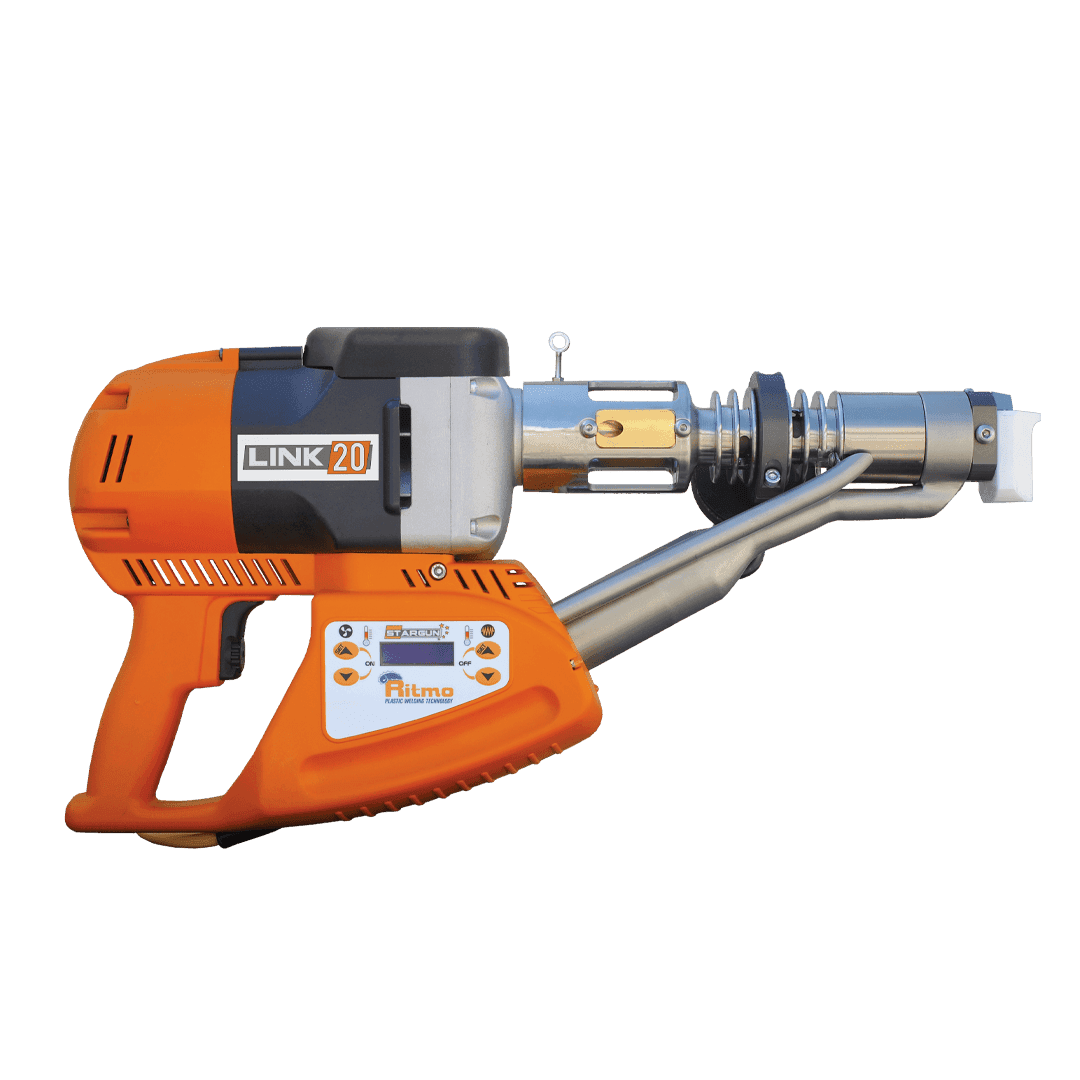
Ritmo Stargun LINK 20 Extrusion Welder 2.2 kg/h
Ritmo · Extrusion Welders and Hot Air Blowers
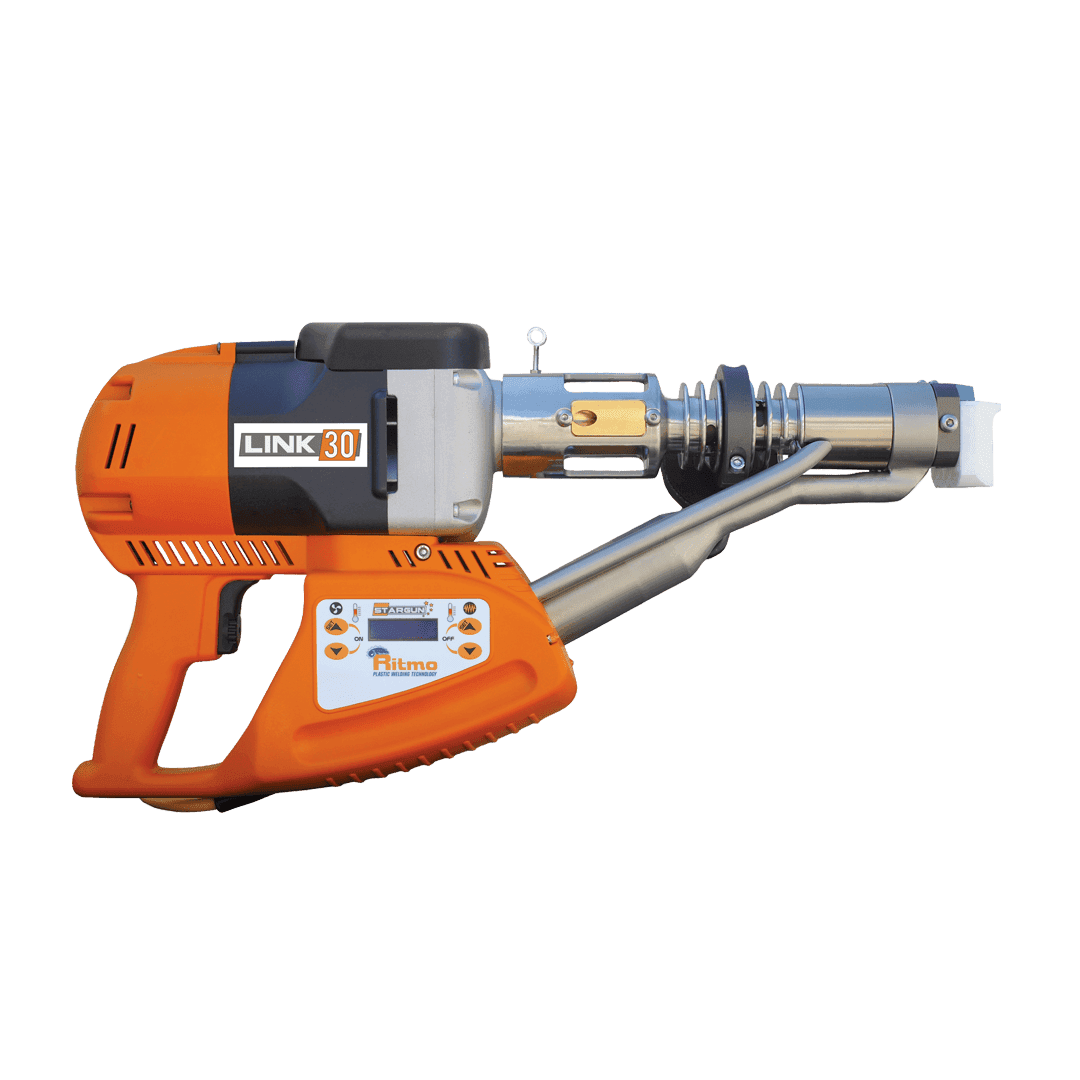
Ritmo Stargun LINK 30 Extrusion Welder 3.2 kg/h
Ritmo · Extrusion Welders and Hot Air Blowers
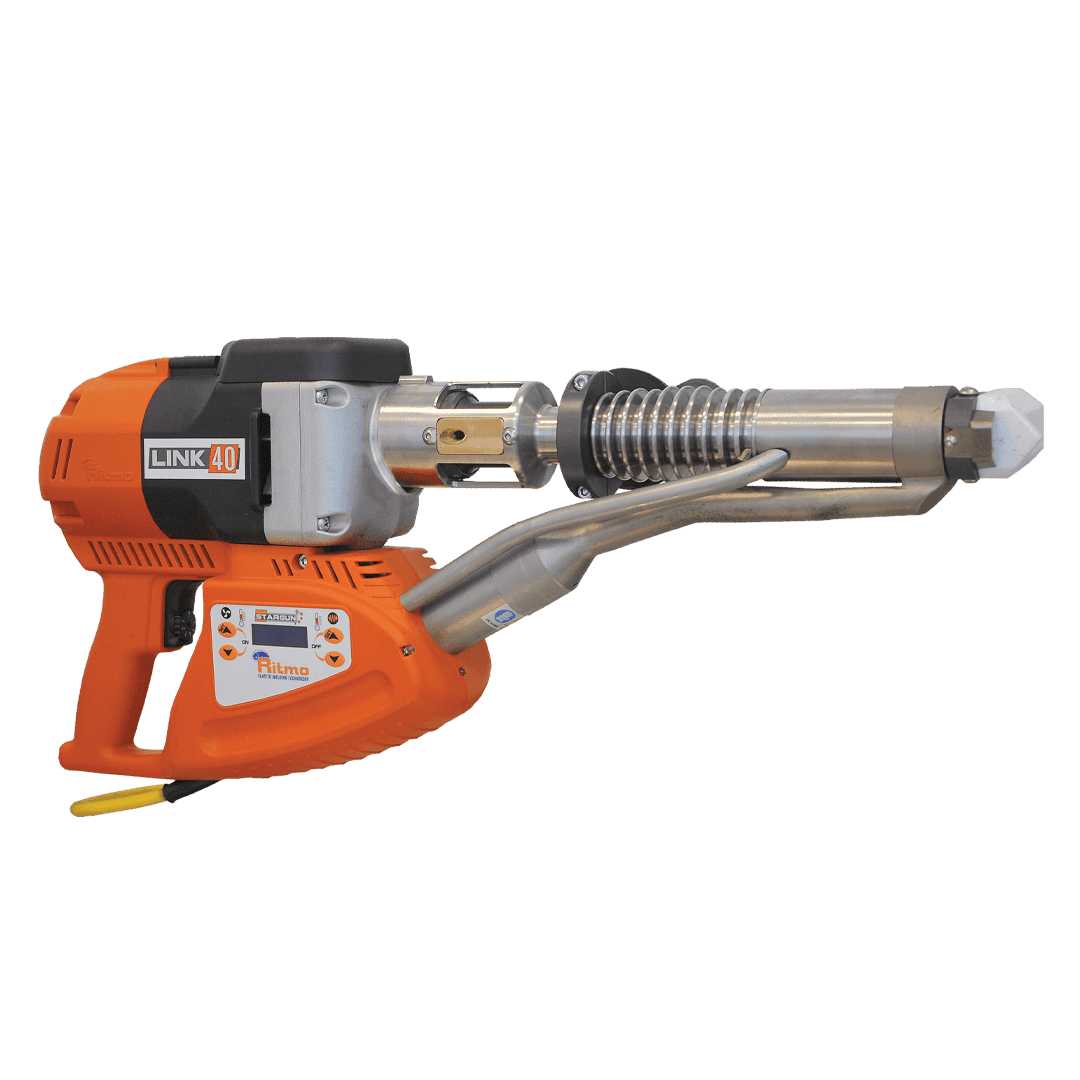
Ritmo Stargun LINK 40 Extrusion Welder 4 kg/h
Ritmo · Extrusion Welders and Hot Air Blowers
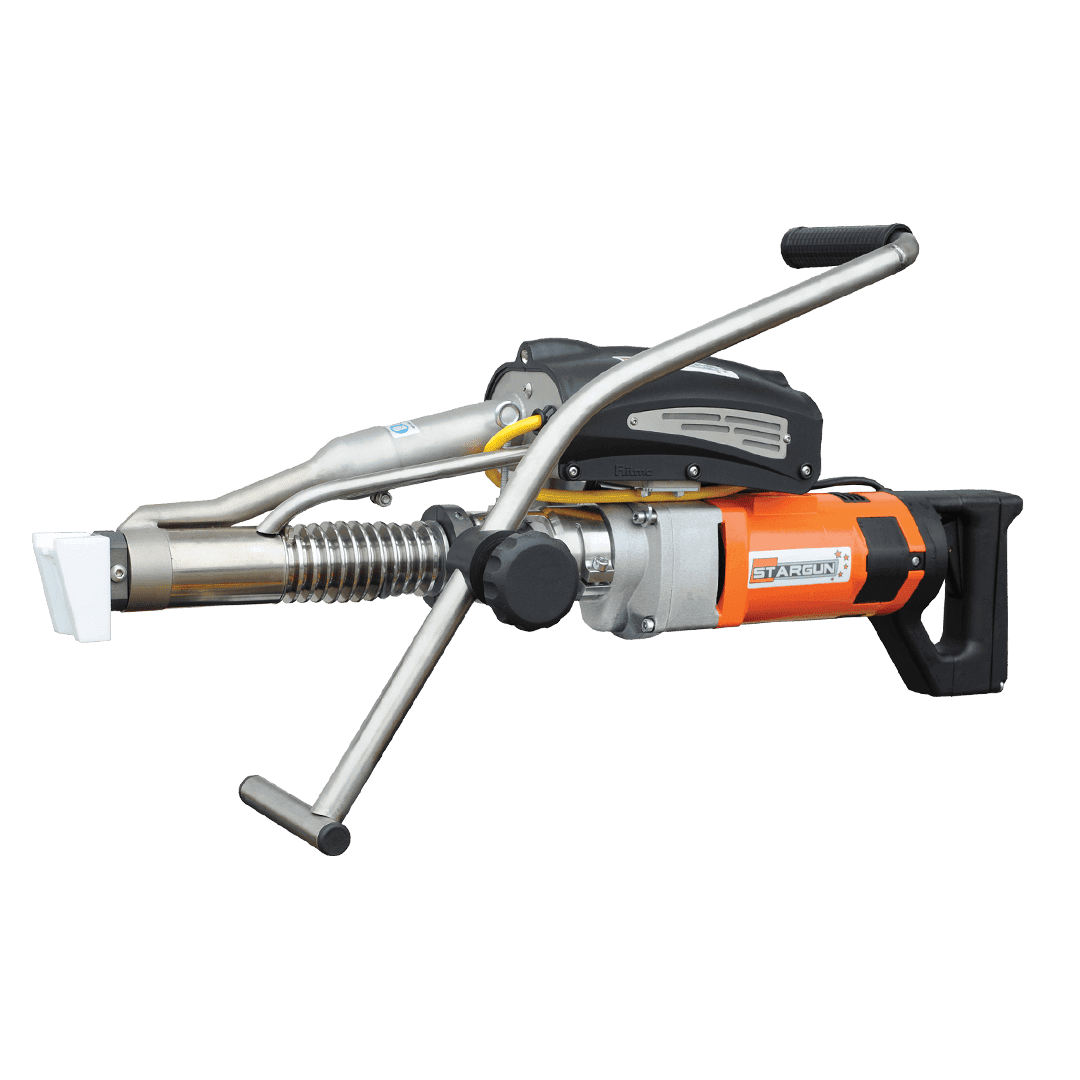
Ritmo Stargun K-SB 50 Extrusion Welder 4.5 kg/h
Ritmo · Extrusion Welders and Hot Air Blowers
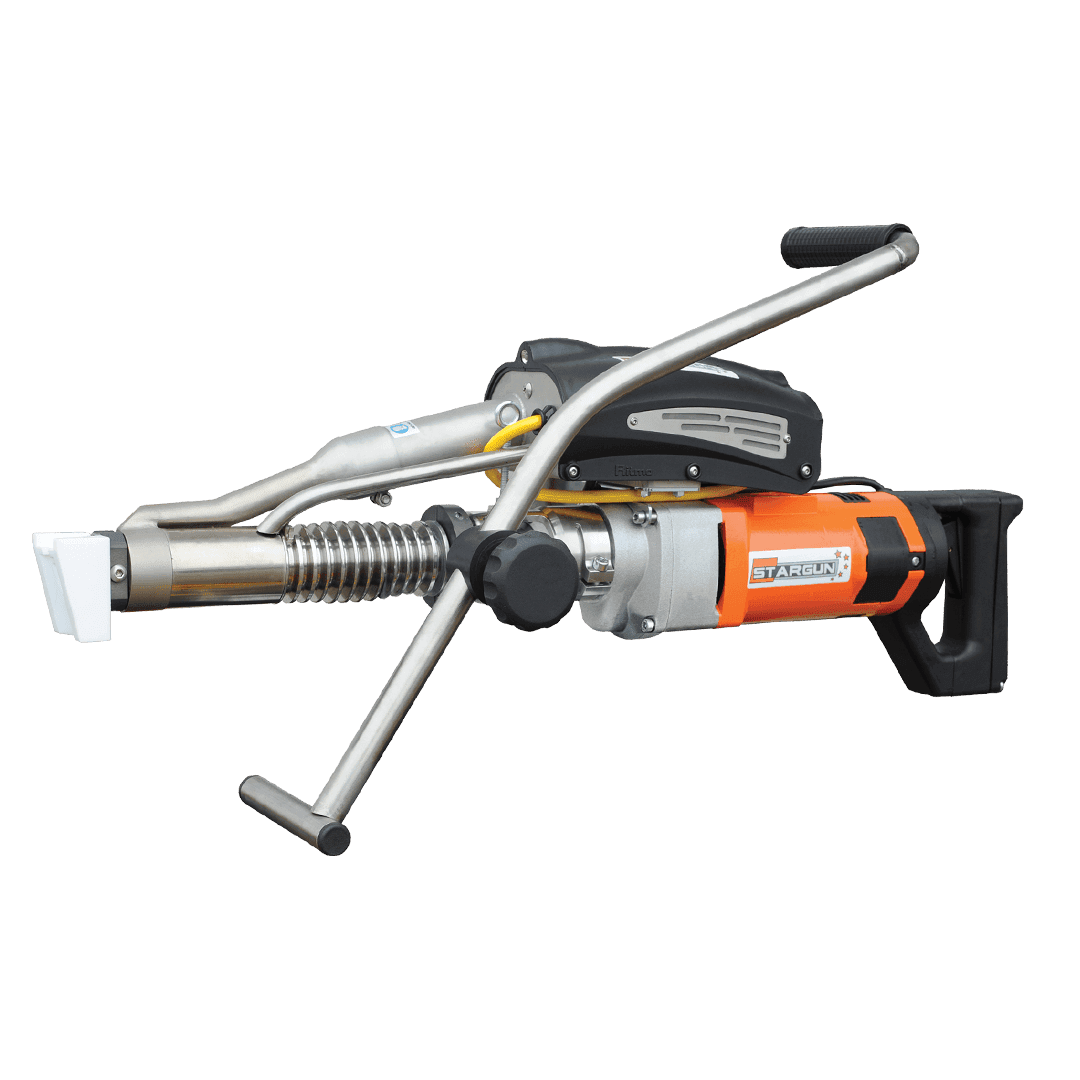
Ritmo Stargun K-SB 60 Extrusion Welder 6.2 kg/h
Ritmo · Extrusion Welders and Hot Air Blowers
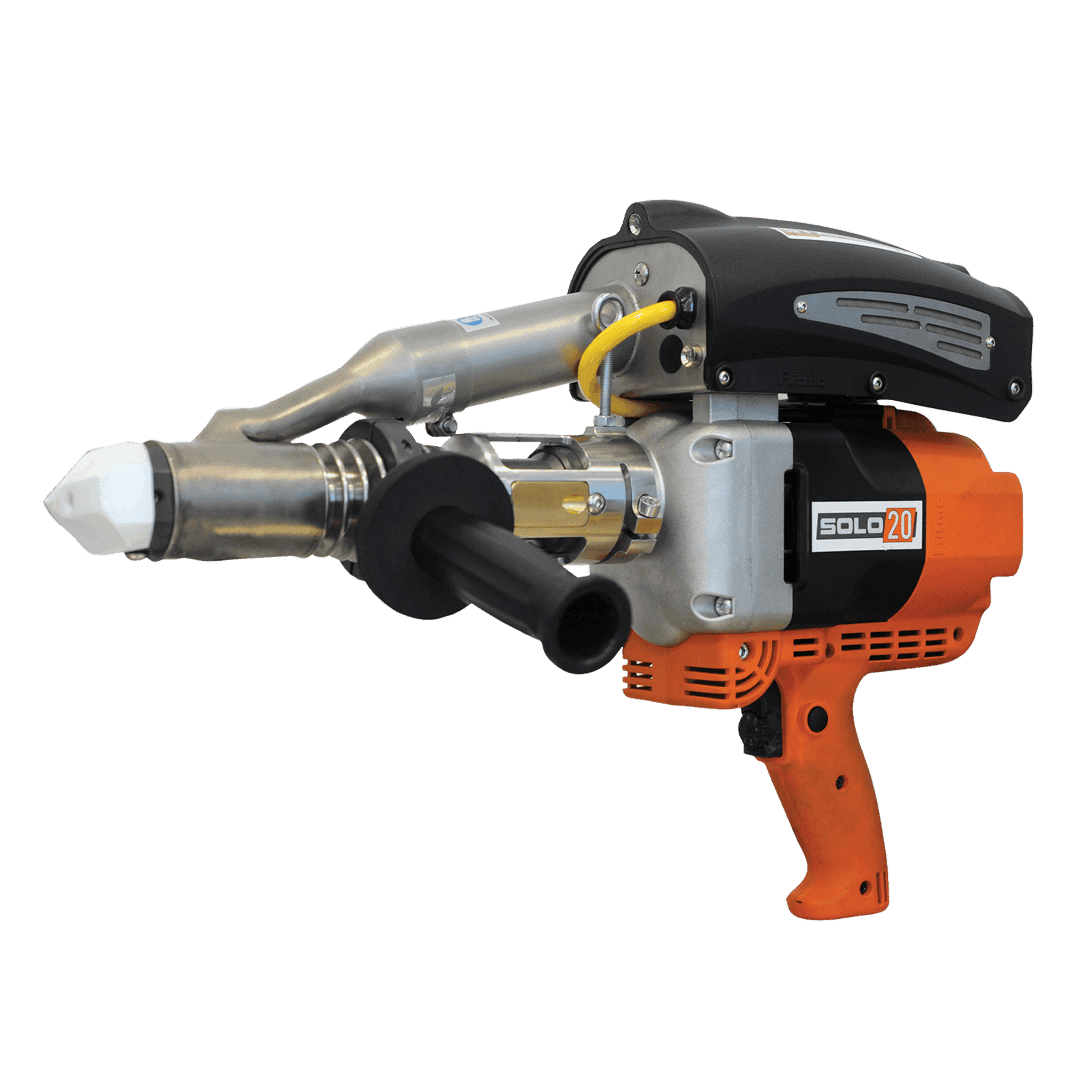
Ritmo Stargun SOLO 20 Extrusion Welder 2.2 kg/h
Ritmo · Extrusion Welders and Hot Air Blowers
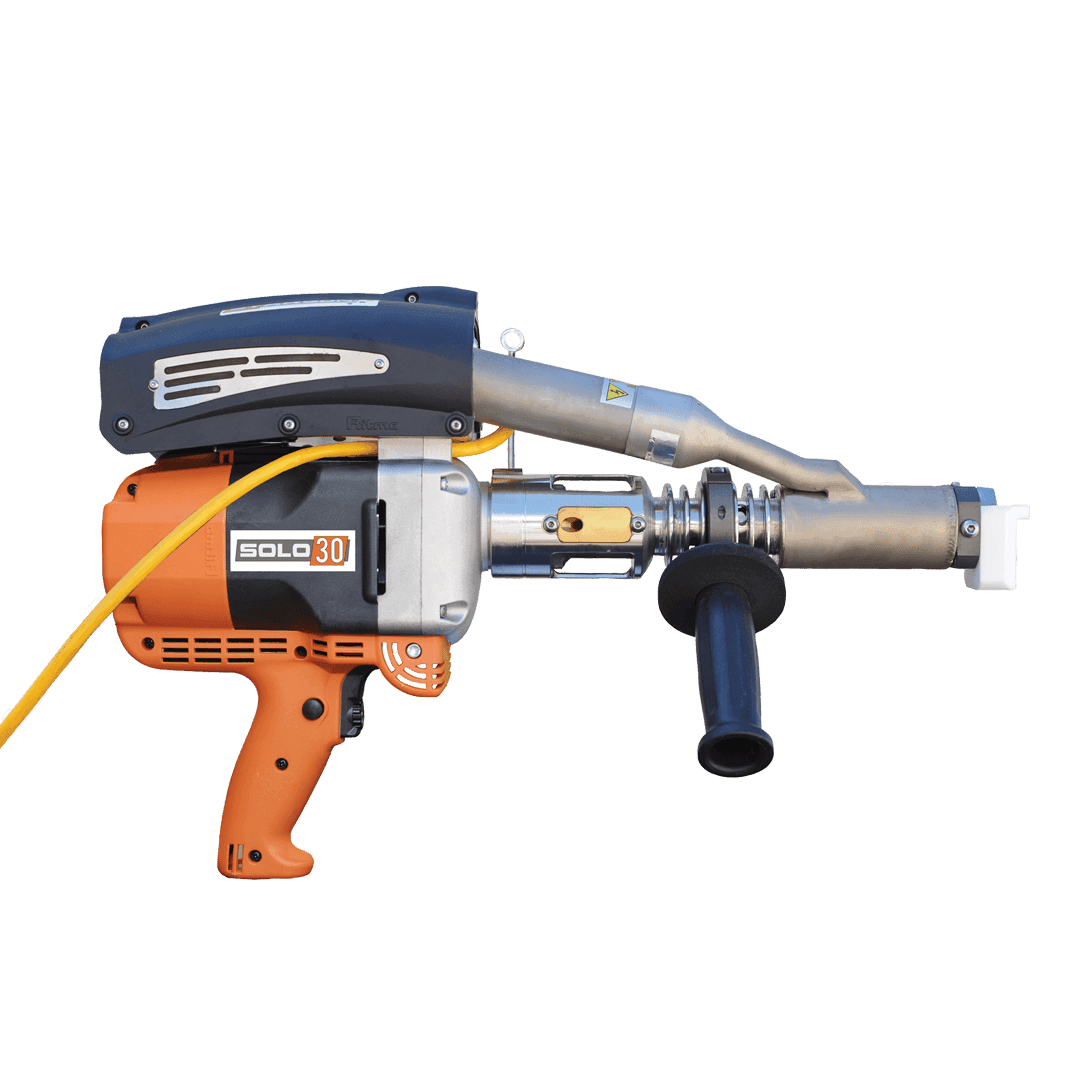
Ritmo Stargun SOLO 30 Extrusion Welder 3.2 kg/h
Ritmo · Extrusion Welders and Hot Air Blowers
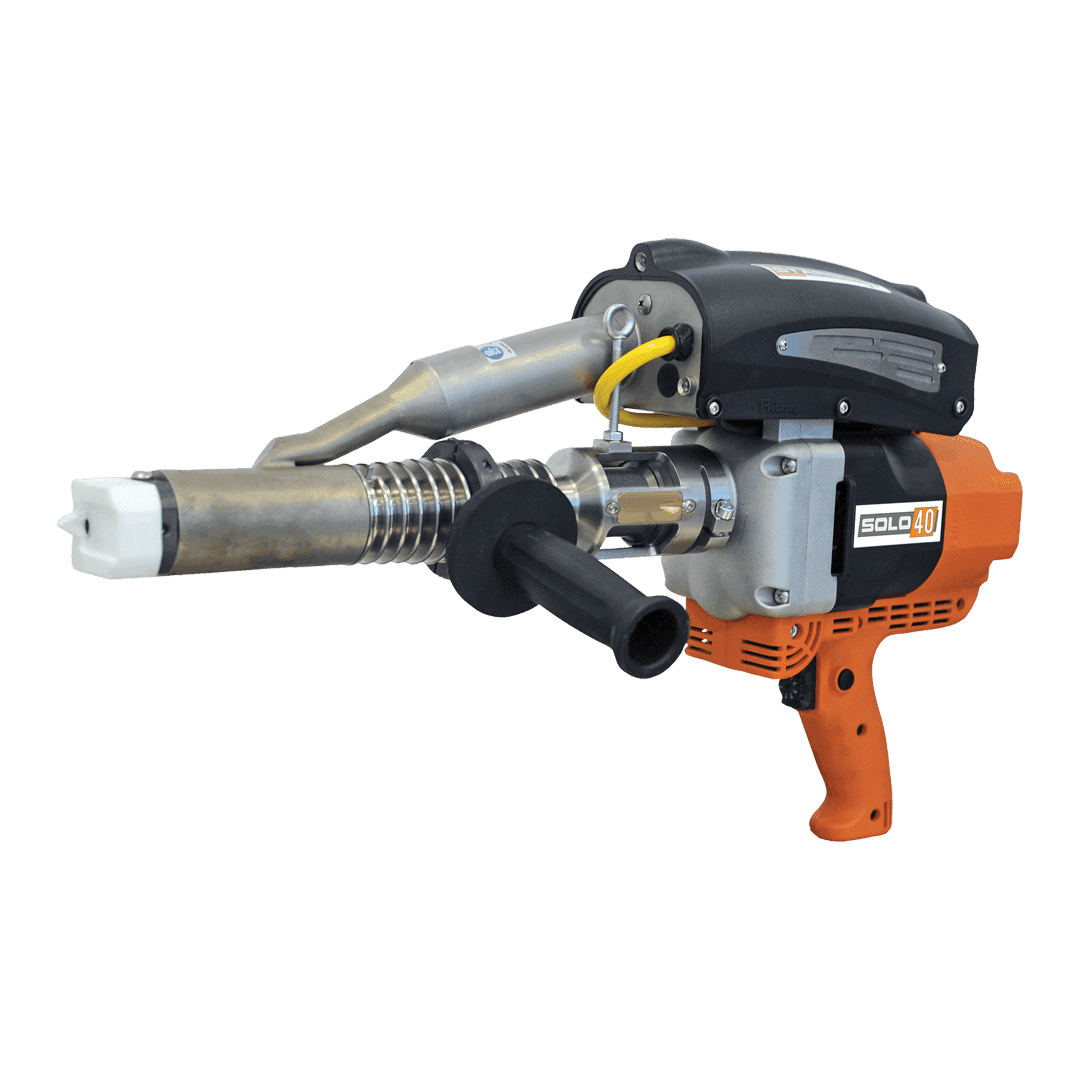
Ritmo Stargun SOLO 40 Extrusion Welder 4 kg/h
Ritmo · Extrusion Welders and Hot Air Blowers
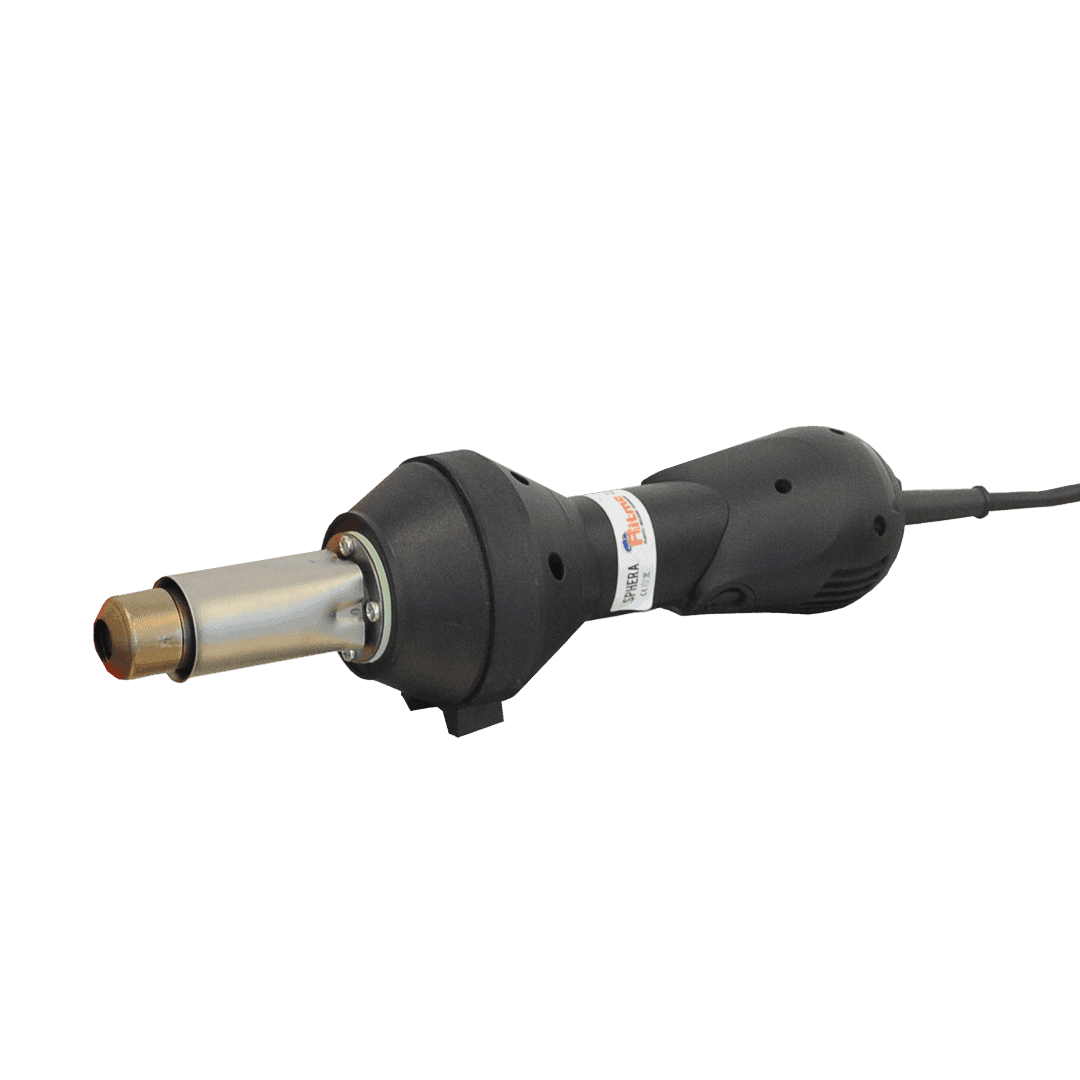
Ritmo Sphera Hot Air Blower 1650 W
Ritmo · Extrusion Welders and Hot Air Blowers
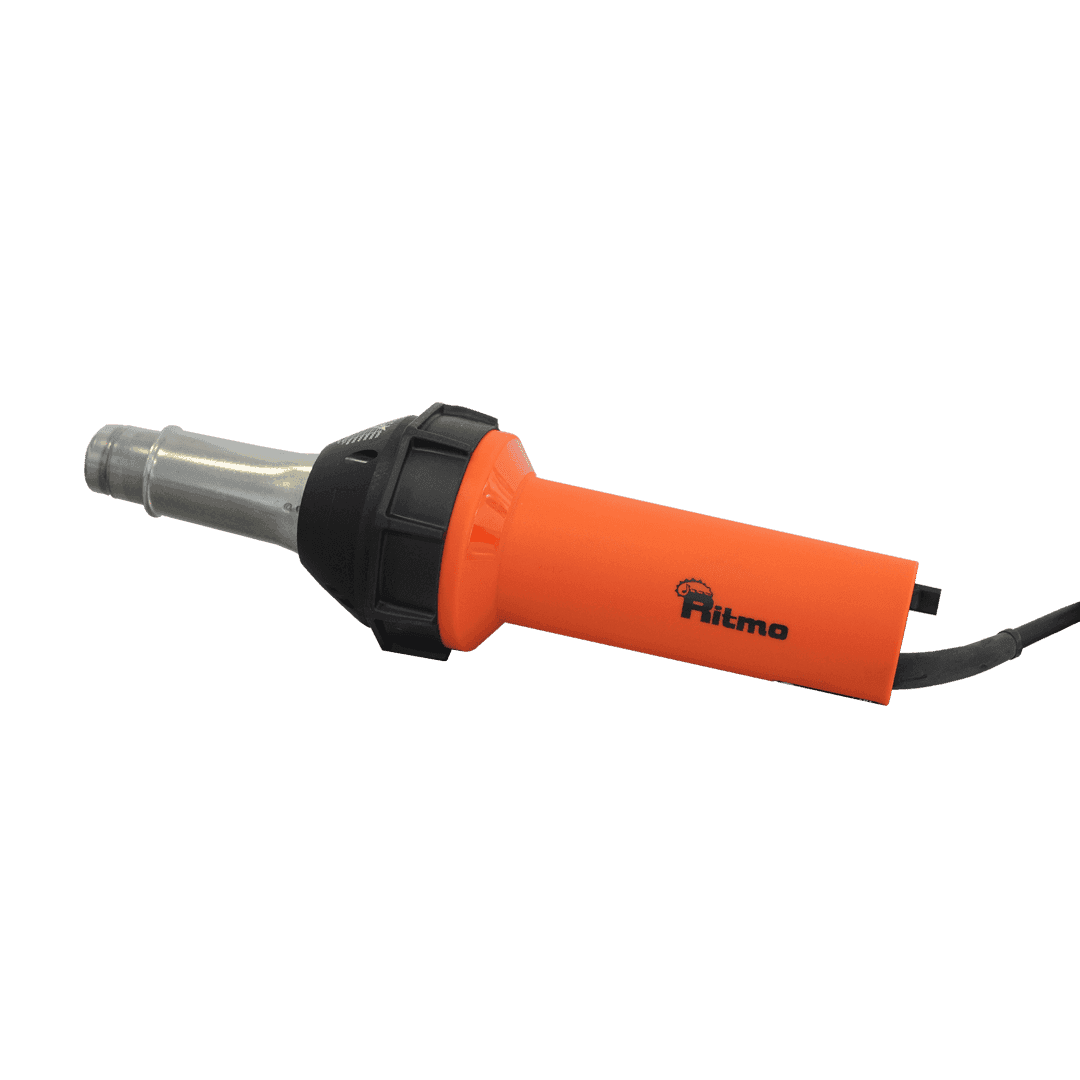
Ritmo HD-PRO V1 Hot Air Blower 1650 W
Ritmo · Extrusion Welders and Hot Air Blowers
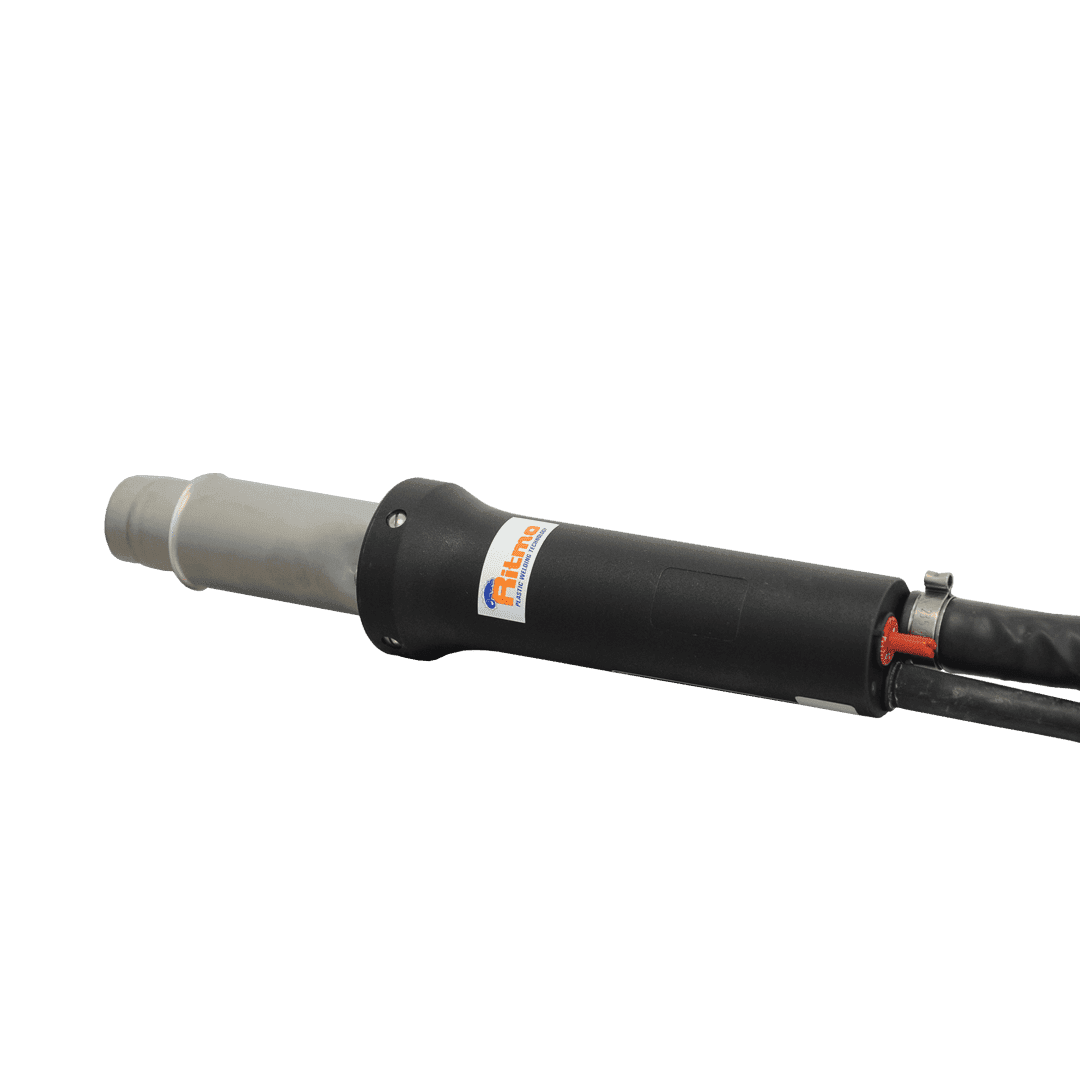
Ritmo Stylo V1 Hot Air Blower (External Air Supply)
Ritmo · Extrusion Welders and Hot Air Blowers
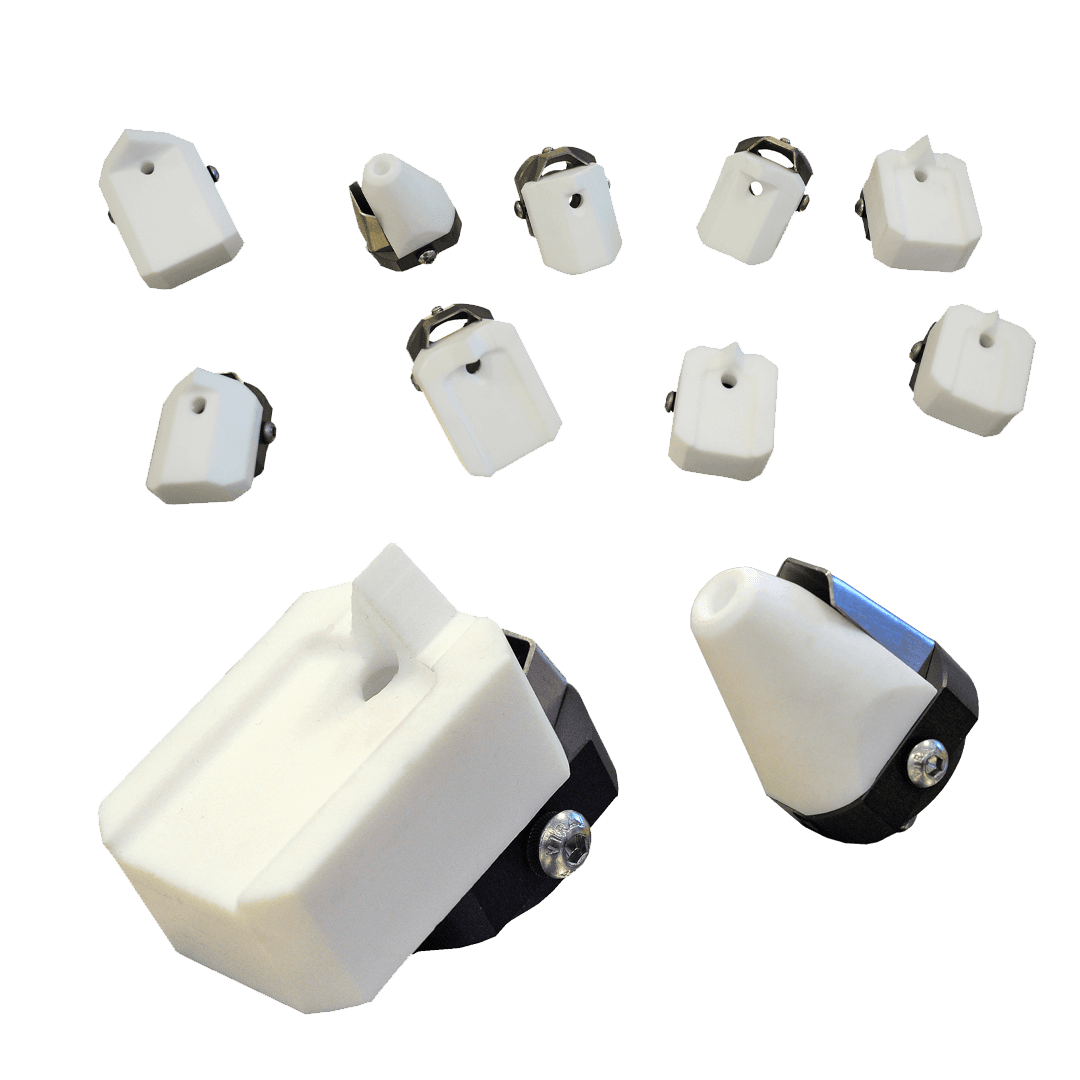
Ritmo Extrusion Welding Shoes
Ritmo · Extrusion Welders and Hot Air Blowers
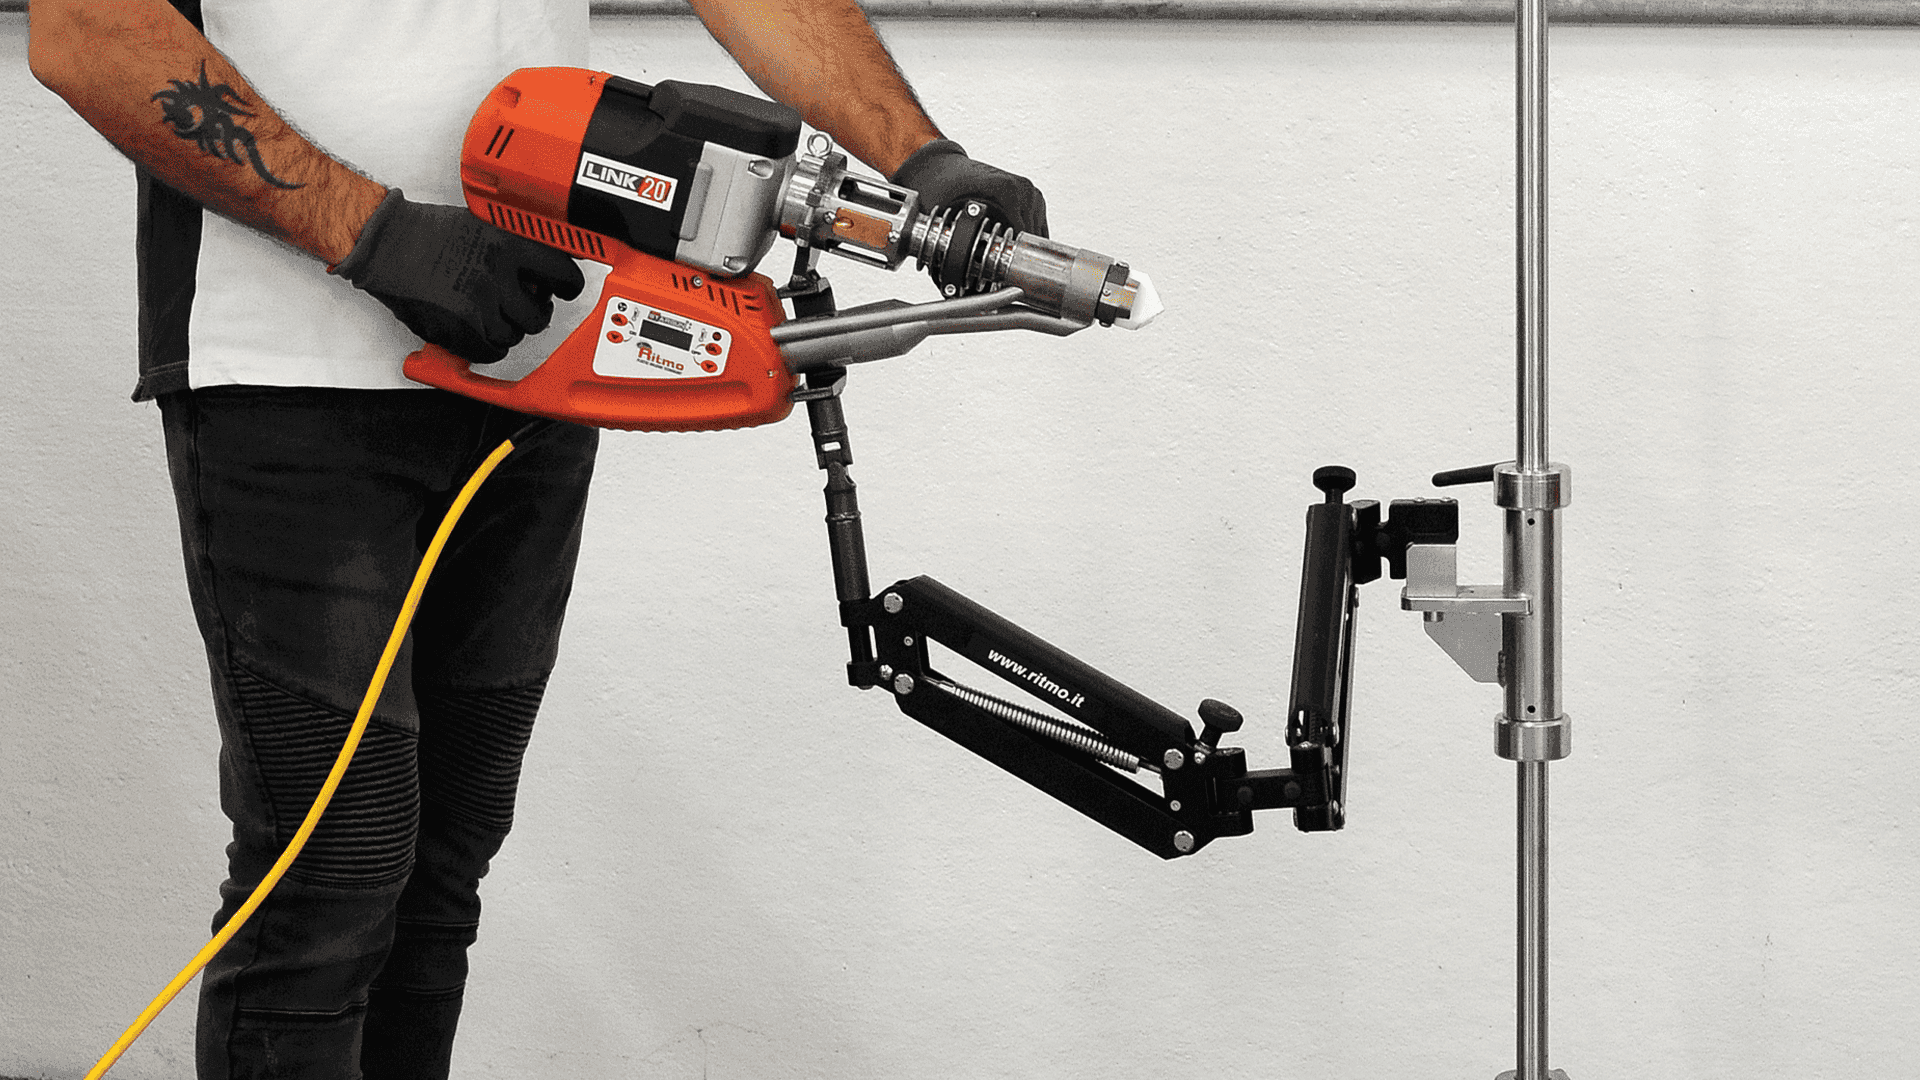
Ritmo Caddy Extruder Carrying System
Ritmo · Extrusion Welders and Hot Air Blowers
Choosing by output and sheet thickness
Two figures decide it: how much material is melted per hour (kg/h) and how thick a sheet can be welded. The UNO's 1 kg/h is enough for repairs and detail work, while continuous fabrication and sheet up to 40 mm calls for the K-SB range; welding thick sheet with an under-sized gun slows the bead down and makes the heat input uneven.
The second distinction is temperature control: on the LINK, K-SB and UNO the air and extrusion temperatures are set separately (dual control), while the SOLO range manages both from one setting. Separate control allows fine tuning across materials and ambient conditions; single control simplifies the machine and lowers the cost.
- Stargun UNO: 1 kg/h, Ø 3-4 mm rod, 1750 W, under 70 dBA
- Stargun LINK 20 / 30 / 40: 2.2-4 kg/h, 1.5-30 mm sheet
- Stargun K-SB 50 / 60: 4.5-6.2 kg/h, 1.5-40 mm sheet, rear handle
- Stargun SOLO 20 / 30 / 40: single temperature control, 2.2-4 kg/h
- Hot air blowers: Sphera, HD-PRO V1, Stylo-V1
- Accessories: welding shoes and the Caddy carrying system
Hot air blowers and accessories
Hot air blowers do two jobs: they preheat the surface ahead of the extrusion weld, and on small repairs they serve as the welding tool on their own. They run to 700 °C, are set on a temperature scale, and stay under 70 dB, which makes indoor work easier; class II (double insulated) construction suits site use.
The welding shoe is the part that gives the extruded material its bead profile and changes with the joint type; with the wrong shoe the bead is under-filled. The Caddy carrying system holds the gun suspended during work and takes the arm load off the operator on long beads.
Frequently Asked Questions
Where is extrusion welding used?
In joining tanks, pools, channels, silos and custom parts fabricated from PE and PP sheet; in geomembrane work; and in pipeline repairs where butt fusion is not possible. Because it lays a lot of material in a single pass on thick sections, it is faster than hot air welding.
How much output do I need?
Sheet thickness and bead length decide it. Up to 20 mm sheet and on intermittent work, 2-3 kg/h is enough; at 30-40 mm and in continuous fabrication the 4.5-6.2 kg/h K-SB models are preferred. Under-sizing the output slows the bead and upsets the heat distribution.
Which rod diameter is used?
Ø 3, 4 and 5 mm depending on the model. Smaller guns take Ø 3-4 mm, the LINK 30 and above take Ø 5 mm. Output figures are generally quoted on Ø 5 mm PE rod; a different diameter changes the figure.
Is the single-control SOLO range enough?
For workshops running continuously on the same material and conditions, yes, and it keeps the machine economical. Where material, thickness and ambient temperature change often, the LINK or K-SB range with separate air and extrusion control gives more controlled results.