Categories
Metal Cutting Saws
This shelf brings together the workshop saws that cut sections, tube and solid bar to length. A metal cutting band saw cuts with an endless blade and offers large capacity; a cold saw cuts with a circular blade at low speed and leaves a clean, burr-free face.
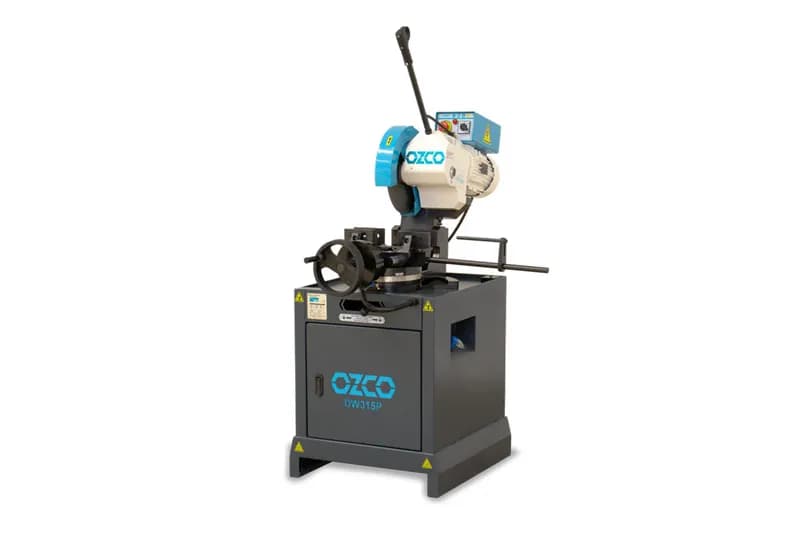
Ozco DW315P Cold Saw 315 mm, Pneumatic Vice
Ozco · Metal Cutting Saws
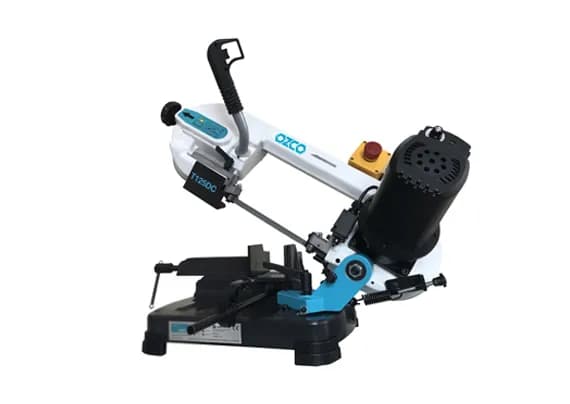
Ozco T125DC Portable Metal Band Saw Ø125 mm
Ozco · Metal Cutting Saws
Ozco T153DC Portable Metal Band Saw Ø153 mm
Ozco · Metal Cutting Saws
Ozco T200 Metal Cutting Band Saw Ø200 mm, Hydraulic Down-feed
Ozco · Metal Cutting Saws
Ozco T225MV Metal Cutting Band Saw Ø225 mm, Hydraulic Down-feed
Ozco · Metal Cutting Saws
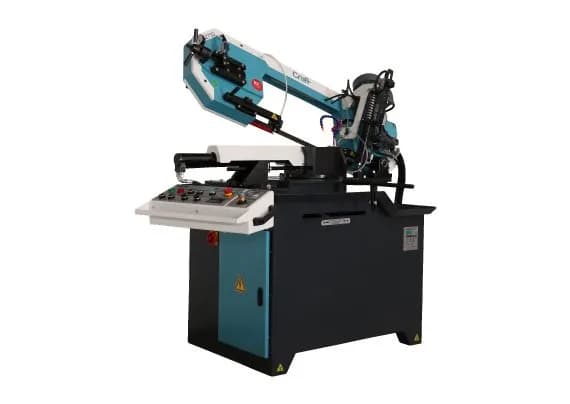
Ozco TS275D Semi-Automatic Band Saw Ø275 mm, Double Mitre
Ozco · Metal Cutting Saws
Band saw or cold saw?
A band saw's thin blade removes little material and cuts large sections: solid bar, heavy profile, bundled tube. The cut is slow but capacity is high.
A cold saw comes first when many tubes and profiles are cut to the same length: the cut is fast, the face is clean and deburring is often unnecessary. Capacity is limited by blade diameter.
Reading cutting capacity
Capacity is given three ways for each angle: round (diameter), square and rectangle (width x height). It drops at mitre; the 45° and 60° figures are on separate rows in the specification table.
Mitres are set one of two ways: the head swivels at the pivot (the stock stays put) or the vice turns. Double mitre models cut both left and right, so both ends of a frame member are cut without turning it over.
Head down-feed and speed control
On manual models the head is lowered by hand; that is where a portable saw's light weight comes from. On hydraulic models the down-feed rate is set and held through the cut, which lengthens blade life and improves the cut.
Inverter models set blade speed steplessly. Stainless and alloy steel want low blade speed, mild steel and aluminium high.
Frequently Asked Questions
Do these saws cut wood?
No, they are built for metal; blade speed and teeth suit metal. Wood band saws are on the Woodworking Machines shelf.
Where do I get a spare blade?
Each saw's blade size (width x thickness x length) is in its specification table; some models list a coded spare blade under options. Other tooth pitches are on the Band Saw Blades shelf.
How do I choose the tooth pitch?
Fine pitch (e.g. 10/14) for thin-walled tube and profile, coarse pitch (e.g. 6/10) for solid and heavy sections. As a rule at least three teeth should be in the cut at once.
When is a portable band saw enough?
On site, for tube and profile up to 153 mm. For production and large sections, hydraulic workshop models are the choice.